Ceramic Valve Solutions for Coal Feeding and Conveying
Reliable isolation and flow control for high-solids coal slurry, dry coal powder, pressurized lock hoppers and pneumatic conveying lines
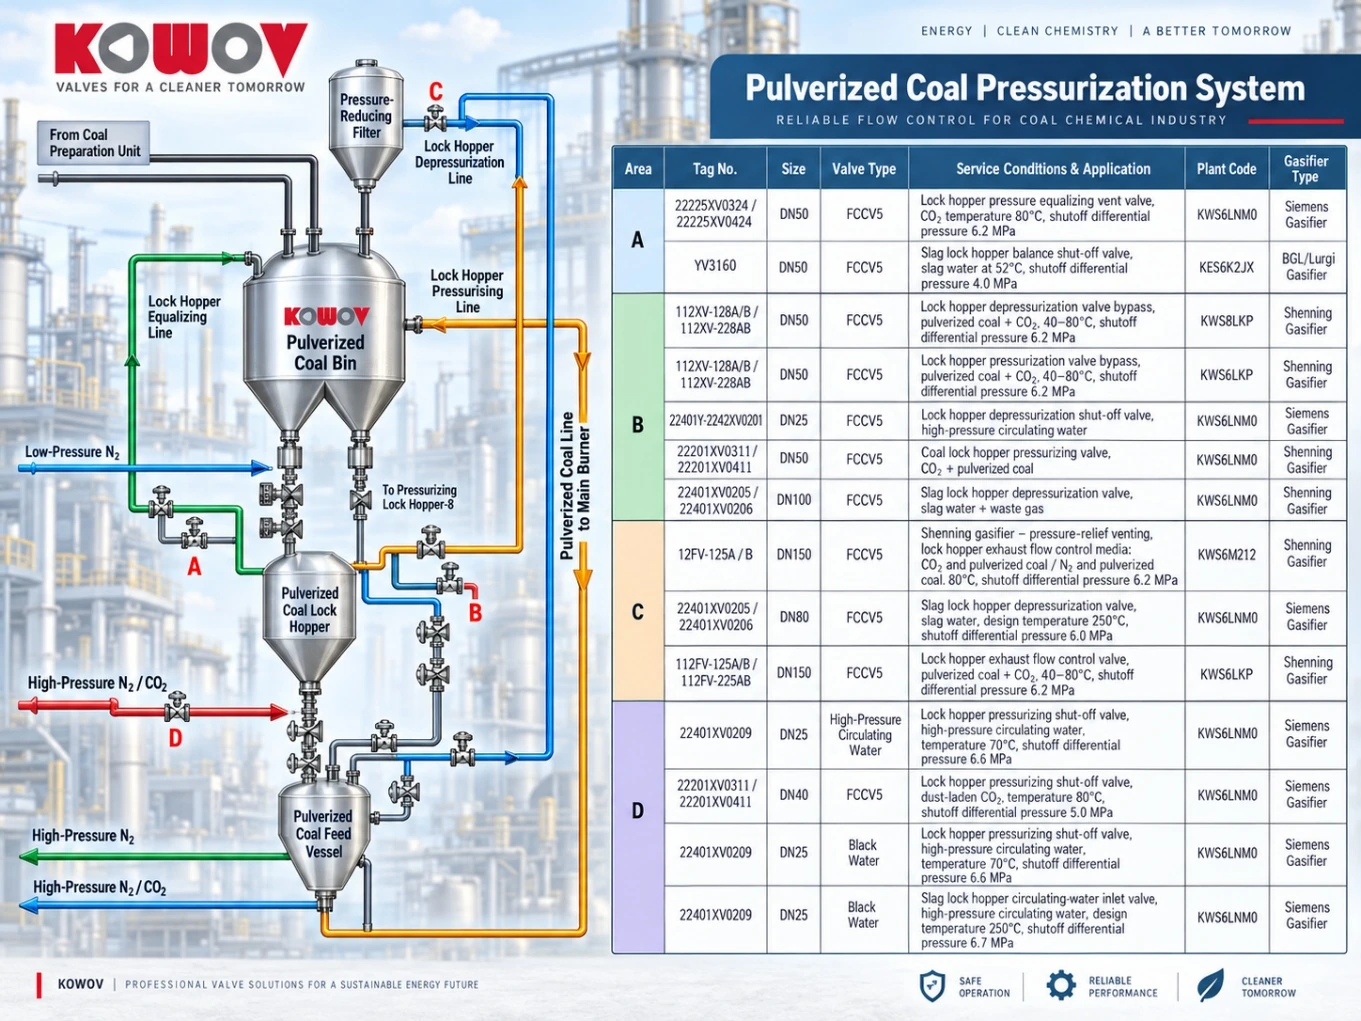
Coal preparation and feeding form the starting point of a coal gasification plant. Depending on the gasification technology, raw coal is prepared either as high-solids coal-water slurry or as dry pulverized coal before being fed into the gasifier
Coal Chemical Industry: Coal Feeding and Conveying Unit
The starting point of the coal chemical process, responsible for conveying raw materials in the form of coal-water slurry or dry pulverized coal to the downstream gasification unit
Operating Conditions
As the starting point of the coal chemical process, the coal feeding and conveying unit handles coal unloading, crushing, grinding and slurry preparation. It delivers qualified coal-water slurry or dry pulverized coal to the gasification unit
Because these media have high solids concentrations and are highly abrasive, reliable valve performance is essential for continuous and stable plant operation
| Parameter | Value | Phase / Classification | Key Characteristic |
|---|---|---|---|
| Process media | Coal-water slurry and dry pulverized coal | Liquid-solid two-phase flow or dry solid particles | Severe abrasive wear |
| Operating pressure | 16-100 bar | Pressure class | ASME Class 150-600 |
| Differential pressure | Up to 135 bar | Nominal size | DN25-DN300 |
| Operating temperature | Below 425°C | Thermal condition | No significant thermal shock |
Process-Media Characteristics
Media in the coal grinding and slurry-preparation unit mainly include coal-water slurry and dry pulverized coal. They contain a high concentration of hard solid particles and may travel at high velocities, creating severe abrasive wear
Powder erosion, material accumulation and valve blockage are common problems. Conventional metal valve bodies and sealing surfaces may suffer rapid erosion and premature failure under these conditions
| Medium Property | Typical Condition |
|---|---|
| Chemical composition | Pulverized coal and coal slurry |
| Corrosive components | Sulfur compounds and trace chloride ions |
| pH | 7-9 |
| Solids content | 55-70% |
| Maximum particle size | Approximately 200-300 μm |
| Particle hardness | Mohs hardness 5-7 |
Summary of Ceramic Valve Applications in Coal Chemical Processes
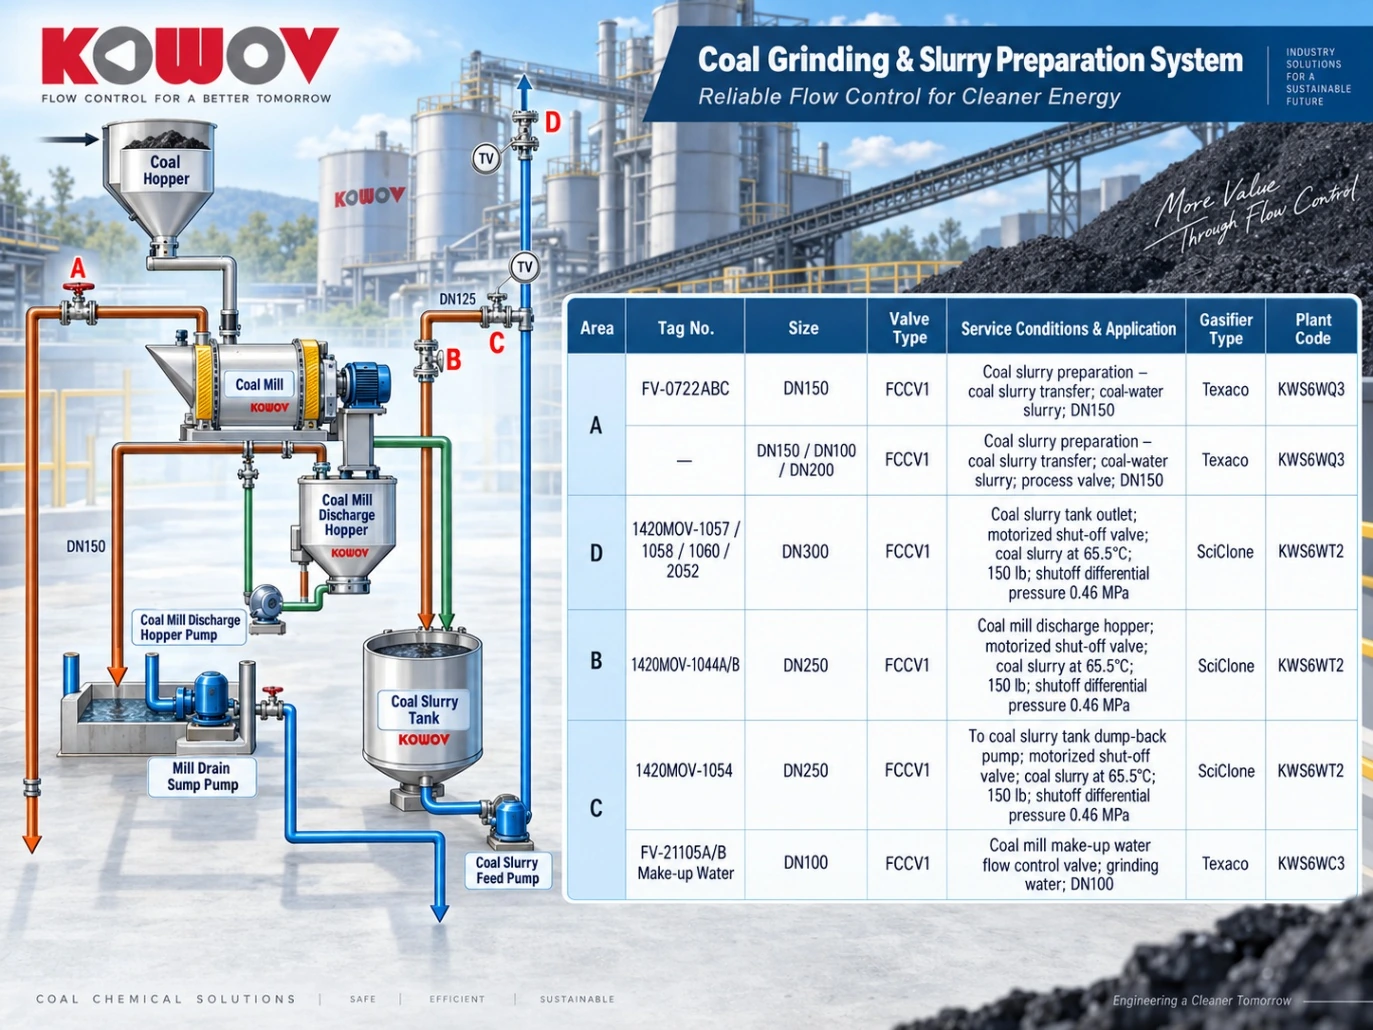
Severe Abrasion and Particle-Erosion Service
For abrasive media such as slag water, coal slurry and pulverized coal, valves use one-piece or segmented ceramic-lined flow passages, with all critical internal components protected by engineering ceramics. The exceptional hardness and mechanical strength of ceramic trim resist particle impact and erosion, preventing sealing-surface wear and internal leakage
Throttling and High-Velocity Erosion Service
For black water and gray water control applications, ceramic V-port ball valves or specially designed ceramic control seats provide stable pressure reduction and precise flow regulation. Ceramic trim extends service life under high-velocity flow and helps prevent valve-seat failure caused by cavitation and erosion
Acidic and Corrosive Service
For acidic water, acid gases and corrosive condensate, chemically stable ceramic materials can replace expensive alloy valves. This prevents premature trim failure and leakage caused by corrosion while improving overall system durability and operational safety
Frequent-Cycling Service
For lock-hopper sequence valves and other frequently operated valves, ceramic hard-seated construction provides excellent resistance to cycling fatigue and particle erosion. The valves maintain reliable shut-off and stable sequence-control performance, substantially reducing maintenance frequency
Overall Value of Ceramic Valve Applications
These operating conditions represent the principal weaknesses of conventional metal valves in coal chemical plants and some of the most mature applications for ceramic valve technology
With exceptional hardness, corrosion resistance and chemical stability, ceramic valves effectively address rapid wear, corrosion and short service life. They significantly reduce inspection and maintenance frequency and are a reliable choice for critical equipment requiring continuous long-term operation
Analysis of Actual Process Pain Points
Existing Valve Materials and Designs
Conventional valves generally use stainless steel or alloy-metal construction, including metal hard-seated ball valves and eccentric rotary valves. These designs cannot withstand continuous erosion and corrosion caused by high-solids, highly corrosive process media
Common Problems with Existing Valves
High-velocity hard particles cause severe erosion and may penetrate internal components. Damage to sealing surfaces results in internal leakage, while aggressive corrosion may damage the trim or valve body and cause external leakage. Particle accumulation in internal clearances may also cause the valve to stick or seize completely
Replacement Frequency and Service Life
Under combined erosion and corrosion, conventional metal hard-seated valves typically last only 6-12 months. At critical operating points, service life may be reduced to just 3-6 months, requiring frequent shutdowns for valve replacement
Losses Caused by Shutdowns and Maintenance
Unplanned shutdowns disrupt production and reduce plant output. Frequent valve replacement increases maintenance costs, while process-media leakage creates environmental compliance risks and potential penalties. High-pressure fluid discharge also poses serious hazards to personnel
Requirement for Long-Term, Reliable Operation
Coal chemical processes involve highly corrosive media, abrasive solid particles and frequent pressure and temperature fluctuations. As critical pipeline control components, valves must provide reliable long-term performance to prevent leakage and equipment failures, reduce unplanned shutdowns, maintain stable process parameters, lower spare-parts and maintenance costs, prevent uncontrolled discharge and material loss, and improve plant safety, environmental compliance and economic performance
Proven Applications of Ceramic Valves in Coal Chemical Plants
Gasification Unit
- Lock hopper depressurization valve
- Lock hopper pressurization valve
- Lock hopper depressurization-line flushing valve
- Lock hopper circulation-pump inlet valve
- Lock hopper circulation-pump recirculation valve
- Other severe-service valves
Coal Feeding and Conveying Unit
- Coal slurry and pulverized-coal conveying-line shut-off valves
- Pulverized-coal vent valves
- Other abrasive-media valves
Slag and Black Water Treatment Unit
- Flash drum level control valve
- Black water flow control valve at the quench-water pump outlet
- Scrubber level control valve
- Hot water tower level control valve
- Black water flow control valve at the slag-pool pump outlet
- Other slurry control valves
Gas Purification and Recovery Units
General-purpose process valves used in shift conversion, ammonia recovery and sulfur recovery units, including:
- Process-line isolation and throttling valves
- Condensate control valves
- Acid gas separator control valves
- Other severe-service control valves
Core Value and Advantages of Ceramic Valve Selection
Coal chemical processes involve severe abrasion, strong corrosion and high differential pressure. With a hardness of HRA 87 or above, engineering ceramic trim provides outstanding resistance to particle erosion and corrosive media. Its inorganic, non-metallic composition also delivers excellent chemical stability and durable sealing performance
Compared with conventional metal valves, ceramic valves can provide a service life 5-10 times longer, significantly reducing maintenance frequency and spare-parts costs. They are an effective upgrade for critical valve positions requiring reliable long-term operation in coal chemical plants
Why Choose Ceramic Valves?
Exceptional Abrasion and Erosion Resistance
Engineering ceramics have a hardness of HRA 87 or above, far exceeding conventional alloy steels. Ceramic valves withstand continuous high-velocity particle impact, abrasion and erosion, significantly extending service life and reducing replacement frequency
Outstanding Corrosion Resistance
Engineering ceramics are inorganic, non-metallic materials with excellent chemical stability. They resist chemical attack from aggressive process media, preventing the pitting, rusting and leakage commonly experienced with metal valves in corrosive service
Mirror-Finished Surfaces Resist Fouling and Jamming
Precision-machined ceramic flow-path surfaces have a mirror-like finish with extremely low particle adhesion. This minimizes solids buildup, scaling and crystallization, helping prevent valve sticking and seizure while reducing maintenance costs
Reliable Operation under Severe Conditions
Ceramic valves provide stable performance under high pressure, elevated temperatures and frequent cycling. Their long-term operating performance remains consistent, ensuring precise flow control and reliable shut-off for continuous plant operation
Conclusion
Ceramic valves are specifically designed to address abrasion, corrosion, fouling and jamming in coal chemical plants. By improving valve reliability at critical operating points, they support efficient long-term plant operation while significantly reducing unplanned shutdowns and maintenance costs
Case Study
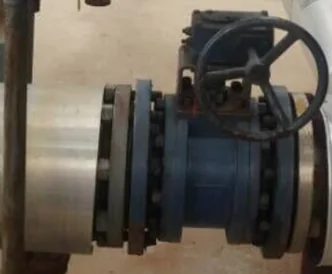
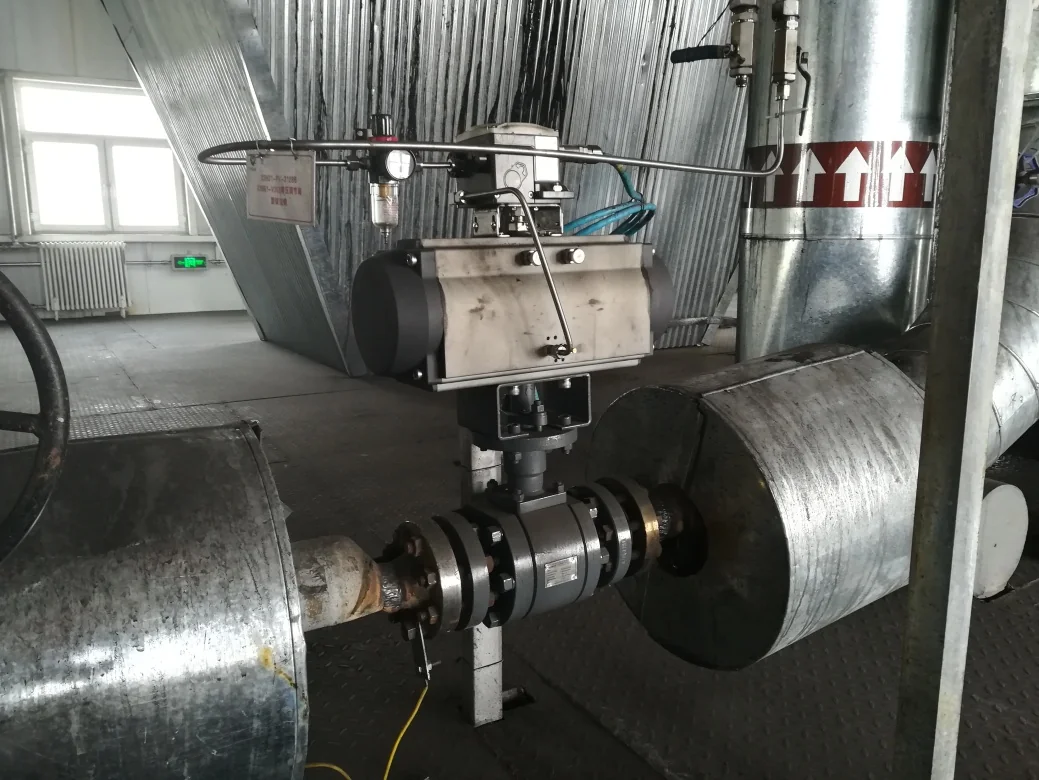
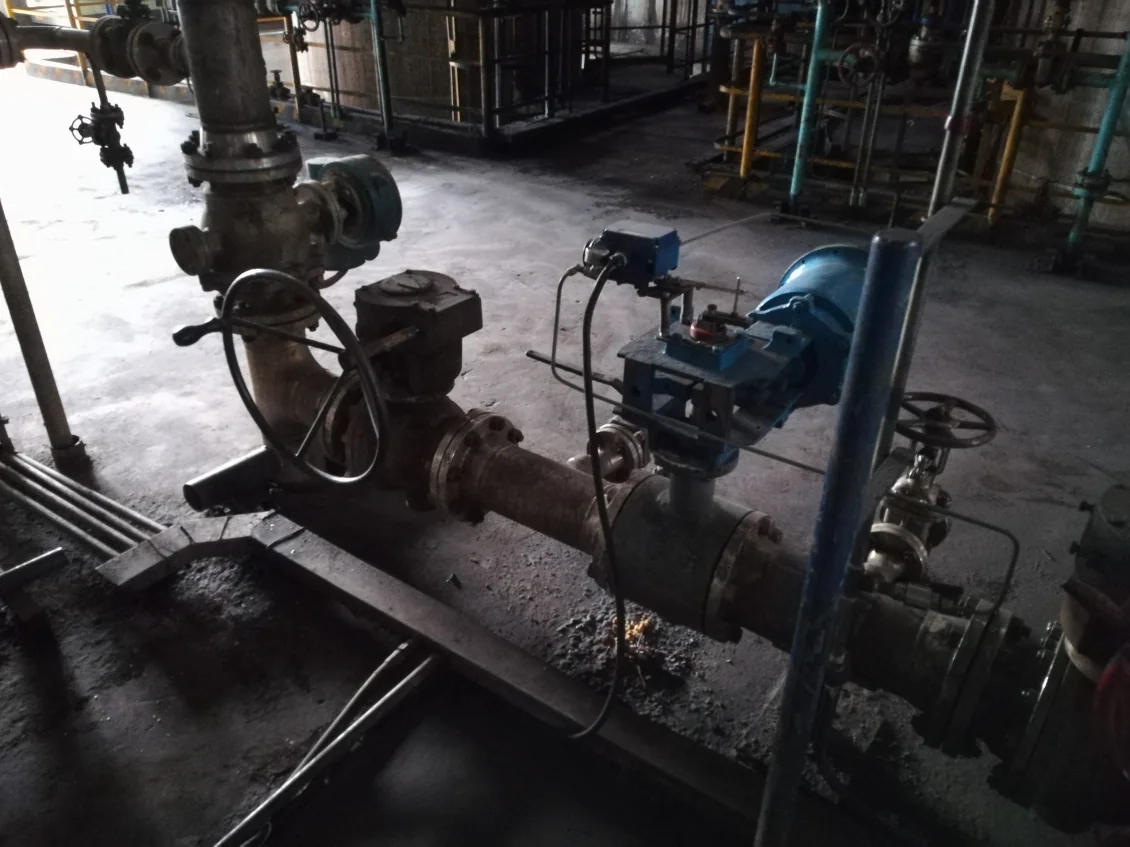
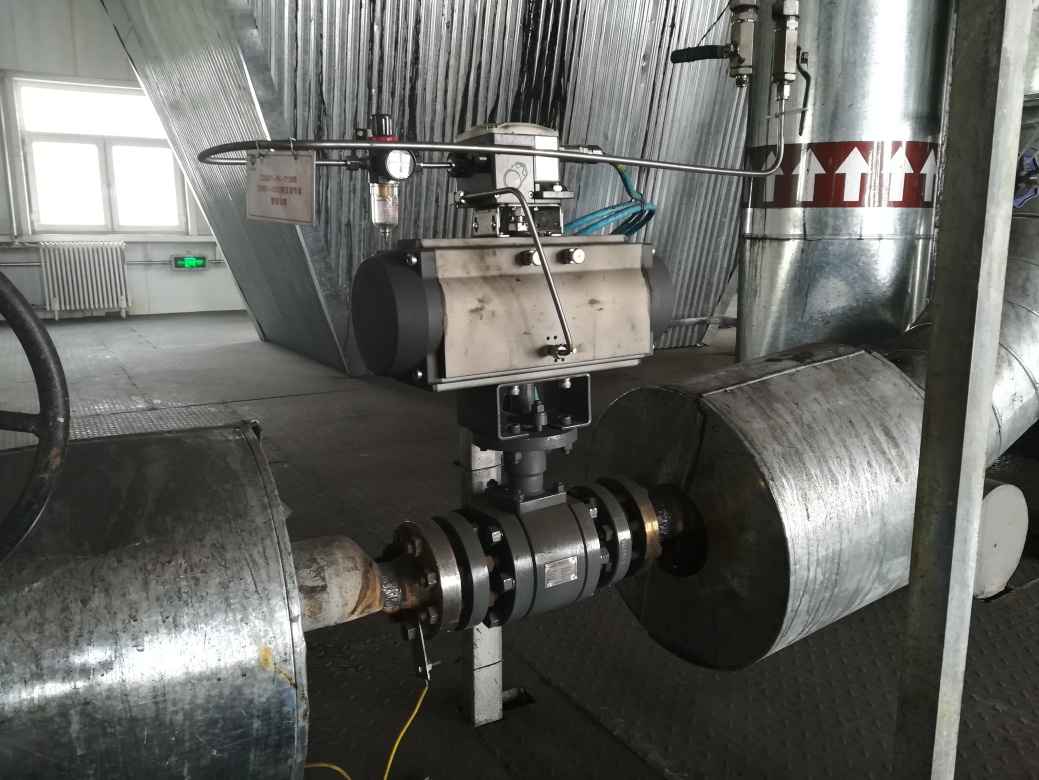
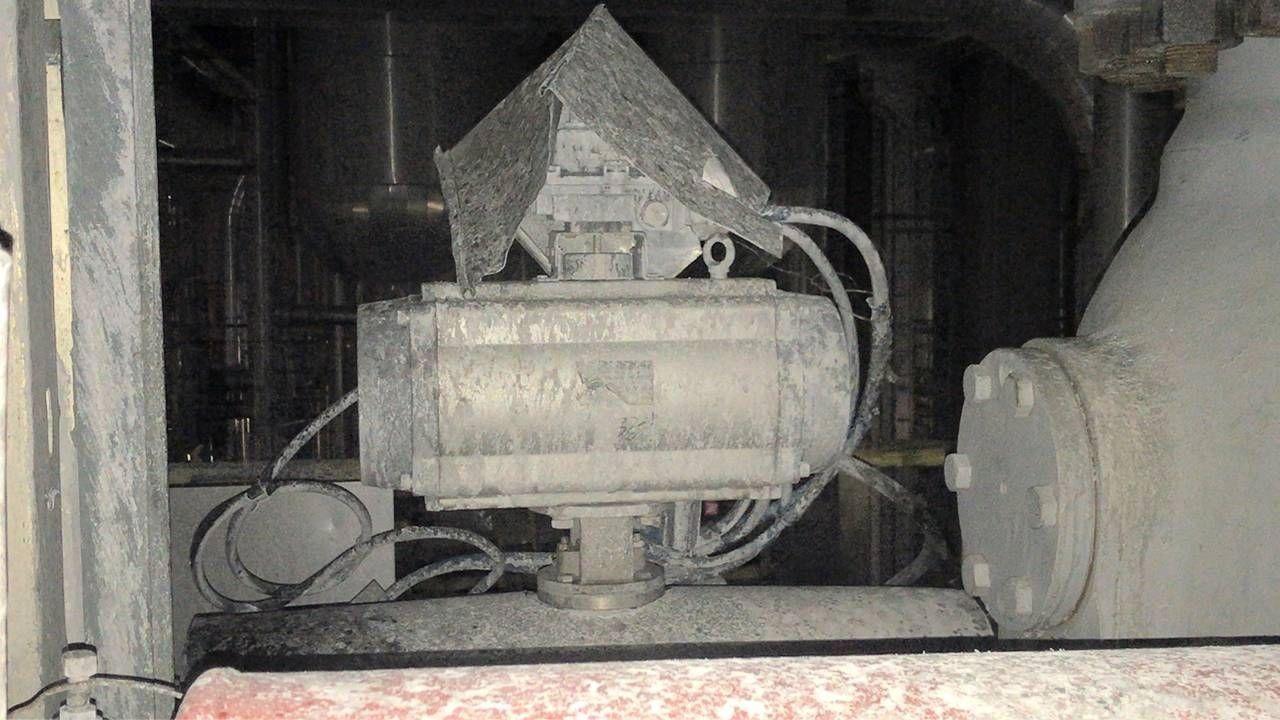
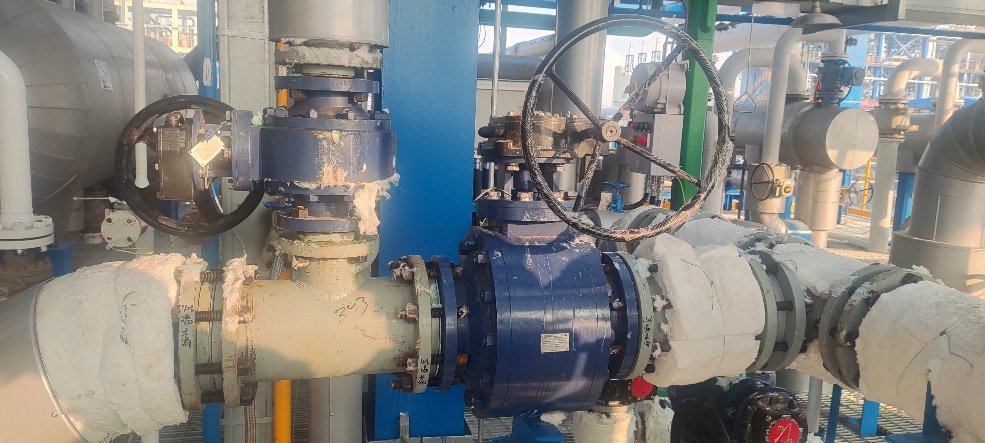
Coal Feeding & Conveying: site photographs
End Users
- China Coal Shaanxi Yulin Energy & Chemical Co., Ltd., China, in service since 2014
- Inner Mongolia Yitai Chemical Co., Ltd., China, in service since 2017
- Shenhua Ordos Coal-to-Liquids Co., Ltd., China, in service since 2017
Application Background
Coal grinding and slurry-preparation systems handle media with extremely high solids concentrations. Ceramic materials provide exceptional resistance to erosion and impact from pulverized coal and coal slurry
The ceramic-lined valve body eliminates the risk of erosion-induced penetration, while smooth operation and stable shut-off help prevent sticking and sealing failure. This addresses the industry-wide problem of frequent valve replacement in pulverized-coal and coal-slurry pipelines
Following the installation of ceramic valves at the Yulin project in 2014, valve service life in the slurry-preparation system increased from 6-12 months to more than two years. The total two-year life-cycle cost per valve decreased by approximately 60-75%
Critical valve positions generated annual savings of several hundred thousand RMB, while the complete slurry-preparation line achieved estimated annual cost reductions of approximately RMB 2-3 million
Conclusion
Minimum recorded service life for ceramic on/off valves: ≥5 years
Commonly Used Products
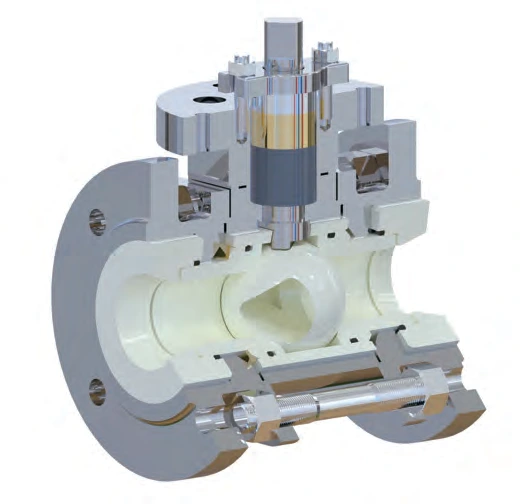
FCCV1
Standard Ceramic Ball Valve
A proven and versatile ceramic ball valve with a classic design, suitable for both on/off and flow-control service. It can be used in most applications with operating temperatures up to 180°C and pressures up to 5.0 MPa, and is particularly effective for corrosive media containing abrasive solids
- Size range: DN15-250 (½″-10″)
- Shut-off class: Class IV or higher
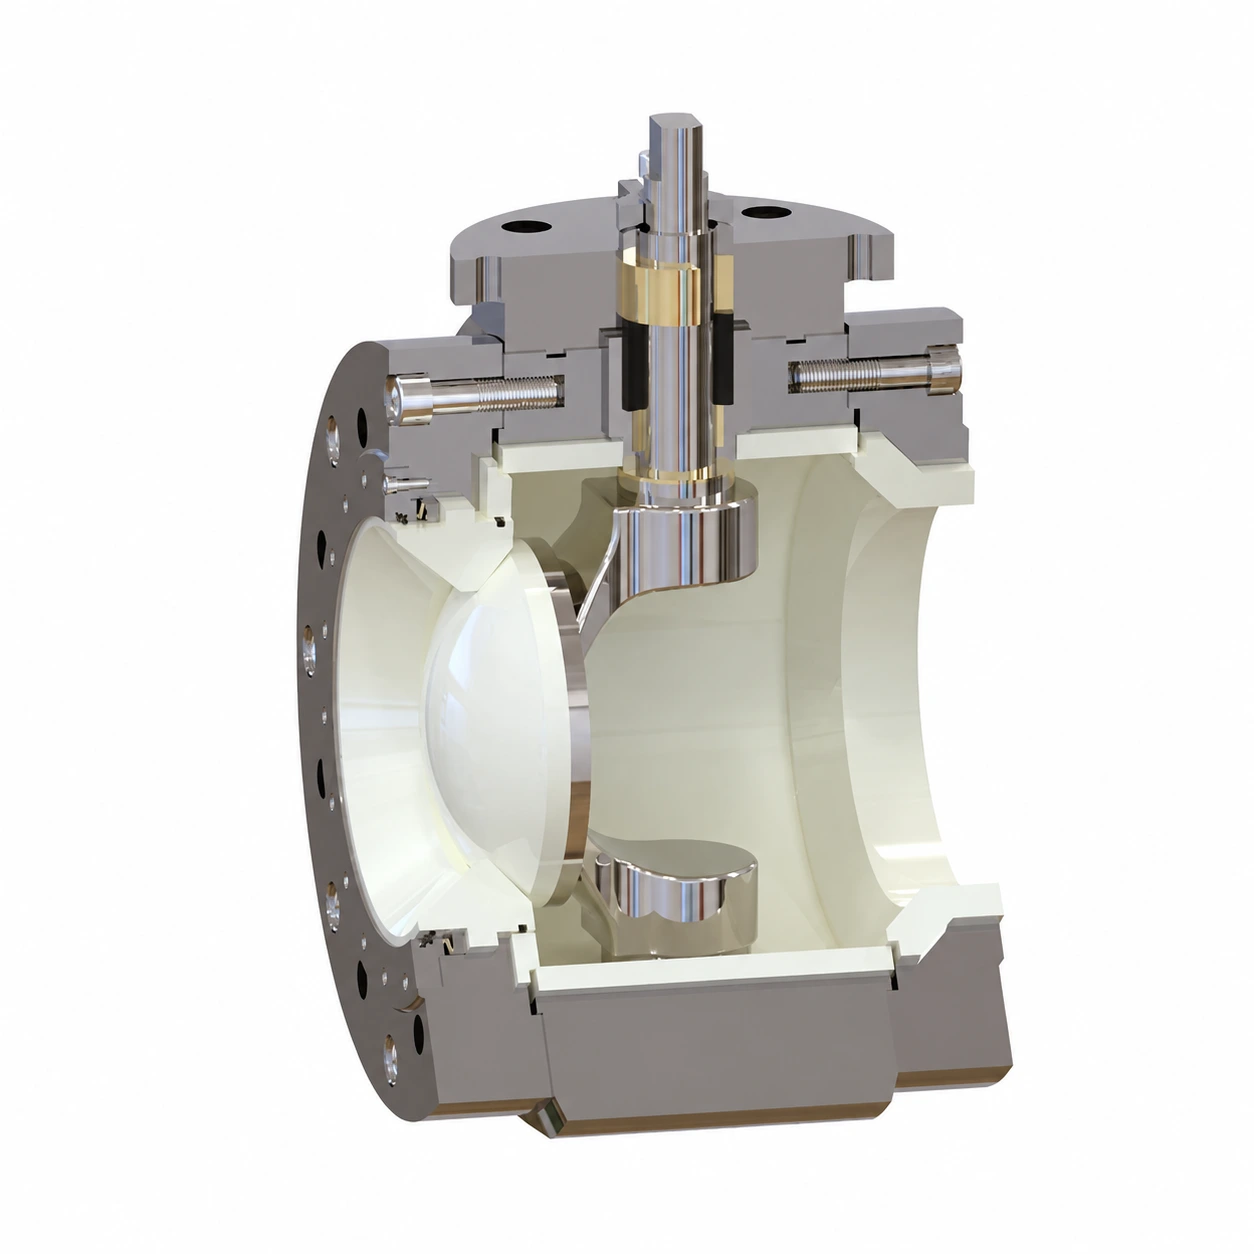
FCRV
Ceramic C-Ball Valve
The valve features a special C-shaped structure. Its ball consists of a C-shaped metal support mechanically connected and securely fitted to a one-piece ceramic ball segment. The ceramic segment protects the metal support from direct erosion by the process medium
The concentric design keeps the ceramic ball segment in continuous contact with the seat during operation, allowing it to scrape deposits from the sealing surfaces and maintain reliable shut-off. It is particularly suitable for media prone to crystallization, scaling, agglomeration, high solids loading and valve jamming. Its cavity-free construction minimizes material accumulation inside the valve
- Size range: DN50-400

FCCV6
Single-Seat Ceramic Ball Valve
This cavity-free ceramic ball valve is designed for reliable control of highly viscous, crystallizing, scaling and agglomerating slurries and mineral slurries. Its unrestricted internal flow path supports smooth, stable, long-term plant operation
The scraping-action valve seat cleans deposited material from the ceramic ball during every opening and closing cycle, helping prevent buildup, sticking and valve seizure
- Size range: DN25-400
Contact Us
Talk to our team about your coal feeding & conveying application
Discuss your application